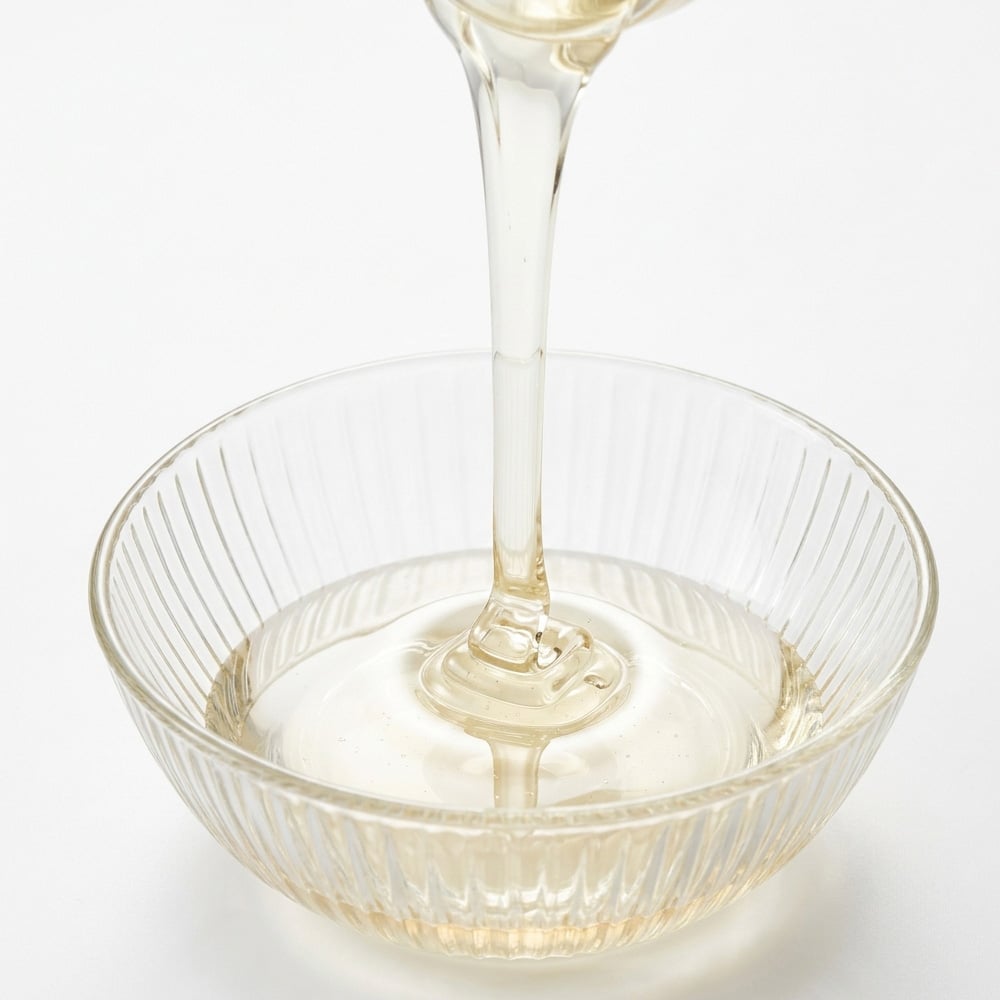
Maltose syrup is a purified, concentrated aqueous solution in which maltose is the predominant saccharide among all sugars present. Produced through enzymatic hydrolysis of starch — typically corn — it delivers a mild, clean sweetness profile with little to no fructose. This compositional characteristic makes it a preferred ingredient in formulations where fructose content needs to be controlled or minimized.
The 80% concentration grade offered in this category is a viscous, transparent liquid designed for industrial food and beverage production systems. Its liquid form supports pumping, metering, blending, and controlled dosing in continuous processing environments. In finished formulations, maltose syrup may contribute sweetness, body, mouthfeel, solids, and texture depending on the recipe and manufacturing conditions.
When evaluating maltose syrup for procurement, understanding the specification range is the starting point — not the endpoint. The parameters that most directly affect downstream production outcomes are DE value, dry solids content, and pH consistency across supply batches. Batch-to-batch consistency in these indicators is a critical purchasing criterion: variation in DE value or moisture content can cause measurable differences in viscosity, sweetness, and final product texture that require reformulation to address.
One observation from production environments worth flagging: maltose syrup viscosity and flow behavior on the production line are not fixed values — they vary with temperature and batch moisture content. If dosing equipment is calibrated against a single reference condition, actual throughput may differ from expected values, particularly during seasonal ambient temperature changes. The operational window is often narrower than laboratory conditions suggest, and this is worth accounting for when setting up equipment calibration protocols.
Maltose syrup serves a broad range of industrial food and beverage applications. Before selecting this ingredient, it is worth asking: what does your specific application actually require from a liquid sweetener — sweetness contribution, body and mouthfeel, fermentable sugar substrate, or solids loading? The answer shapes which specification parameters to prioritize in supplier evaluation.
In hard-boiled candies, toffees, chewing gum, and fondants, maltose syrup contributes body and controlled sweetness. Its moderate viscosity profile supports processing in confectionery cooking and forming equipment. The low fructose content reduces hygroscopicity concerns relative to some alternative liquid sweeteners, which can matter for hard candy shelf stability in humid environments.
In the beverage sector, starch sweetener selection is often driven by texture, mouthfeel, and fermentability requirements rather than sweetness intensity alone. For soft drinks, protein drinks, and juice-based products, maltose syrup provides a calorie-contributing sweetener base with a less intense sweetness impact compared to high-fructose alternatives. Its liquid handling format is compatible with continuous beverage filling line dosing systems. For beverage formulation teams, verifying the viscosity behavior of the specific grade at your processing temperature is recommended before finalizing dosing equipment settings.
Maltose syrup can serve as a malt substitute in beer production, providing a fermentable sugar substrate for yeast. The high maltose content — the DP2 fraction at 46–60% — aligns with the sugar profile that brewing yeast efficiently metabolizes. This makes it a practical adjunct for adjusting wort composition or supplementing fermentation capacity without requiring additional malt processing infrastructure.
In jams, sauces, canned food, and processed meat products, maltose syrup functions as both a sweetener and a solids and viscosity contributor. Its controlled sweetness profile and liquid form allow for precise addition in batch cooking and mixing processes. In these applications, the consistent DE value across supply batches is particularly relevant, as variation affects final product viscosity and mouthfeel in measurable ways.
Effective grade selection for maltose syrup involves matching specification parameters to application requirements — not simply accepting the nearest available grade. For R&D teams working on new formulations, identifying which specification indicator most directly affects the target product attribute is worth doing before large-volume procurement commits.
For brewing adjunct applications, the DP1-to-DP2 ratio and DE value are more relevant selection criteria than Brix alone. For texture-critical confectionery applications, the DE value range and its effect on crystallization tendency at processing temperatures should be verified against production line conditions. For beverage applications, mouthfeel contribution and dissolving behavior in your processing water temperature and pressure conditions are the parameters to evaluate first.
A practical note for procurement teams managing multiple ingredient suppliers: mixing maltose syrup batches from different supply sources — even when both nominally meet the same specification — introduces DE value variation that can affect finished product viscosity, sweetness, and texture in ways that are difficult to attribute without full batch traceability. Establishing a consistent single-source supply relationship for a given production line reduces this risk over time and simplifies batch rejection investigations when they do occur.
For production lines integrating maltose syrup for the first time, a pre-production dissolving and flow test at actual water temperature and equipment settings is advisable. Storage conditions also affect usable product quality: liquid syrups stored in warehouses with inadequate temperature or humidity control can develop viscosity drift or microbial risk that is sometimes attributed to transit damage — clarifying storage requirements with your supplier and aligning them to warehouse conditions before confirming volume commitments is a step worth including in supplier onboarding procedures.
Bulk maltose syrup procurement typically sits within larger starch sweetener and liquid ingredient sourcing strategies for food and beverage manufacturers. International buyers in this category evaluate suppliers on three dimensions: specification consistency across batches, export documentation and compliance capability for target import markets, and the ability to co-supply complementary ingredients to reduce multi-vendor management complexity.
From a quality assurance standpoint, requesting supplier documentation that references recognized food-grade liquid sweetener specifications — including purity parameters, microbiological limits, and analytical test methods — helps verify whether a supplier's quality management system operates against defined benchmarks. Consider citing a relevant quality or testing standard that applies to food-grade glucose and maltose syrups in your evaluation criteria, and note its applicability scope against the regulations in your target market. (Specific standard references should be verified against current regulations before use in procurement documentation or product labeling.)
For cross-border procurement, a supplier with an established export track record to markets including North America, Southeast Asia, and South Asia demonstrates multi-market documentation experience — reducing onboarding friction for buyers sourcing internationally from China for the first time. Familiarity with phytosanitary certificates, COA formats accepted in destination markets, and logistics coordination for bulk liquid shipments in drums, flexibags, or IBC totes is directly relevant to procurement planning timelines.
Buyers in the beverage and condiment sectors who also source caramel color or related starch-derived ingredients may find value in evaluating suppliers with multi-product capability. Co-sourcing maltose syrup alongside caramel color from a single supplier can consolidate logistics coordination, reduce documentation management overhead, and streamline annual quality audit scope — particularly relevant for buyers managing lean procurement teams.
 EN