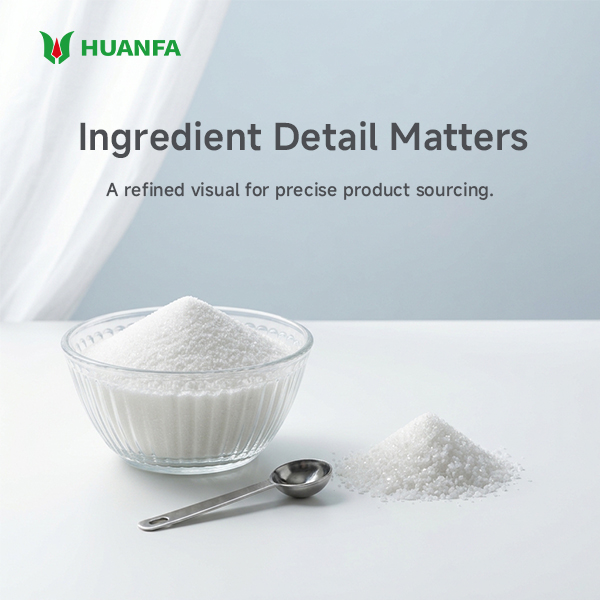
Granular Sorbitol Food Grade stands as a cornerstone ingredient in modern food formulation, prized for its unique combination of sweetness, humectancy, and chemical stability. Unlike liquid sorbitol, the granular form offers superior handling, storage, and blending characteristics, making it indispensable in dry applications such as sugar-free confectionery, powdered drink mixes, and instant desserts. As a polyol, sorbitol is metabolized independently of insulin, catering to diabetic-friendly and low-glycemic product lines. Its non-cariogenic nature supports oral health claims, aligning with consumer demand for functional foods. In bakery systems, granular sorbitol extends freshness by retaining moisture, while in chewing gum it provides a smooth, cool mouthfeel and excellent plasticizing action. From a regulatory perspective, it is approved as E420 in the European Union and recognized as GRAS by the FDA. Our production process begins with high-quality corn starch, hydrolyzed into glucose syrup, then hydrogenated under controlled pressure and temperature to yield sorbitol with consistent purity. The molten sorbitol is spray-crystallized into uniform granules, screened to precise mesh cuts, and tested for residual sugars, moisture, and particle size. This rigorous approach ensures that every shipment of our Granular Sorbitol Food Grade performs identically in your production line, batch after batch, supporting your brand’s quality promise in over 60 countries.
12
Aug
24
Sep
17
Sep
14
Sep
 EN