Pharmaceutical Polyol Excipient Supplier | USP/EP-Compliant

All Categories
Pharmaceutical Polyol Excipient Supplier – High-Purity Sorbitol, Maltitol, Xylitol & More

Pharmaceutical Polyol Excipient Supplier – High-Purity Sorbitol, Maltitol, Xylitol & More

As a leading Pharmaceutical Polyol Excipient Supplier, we deliver premium-grade sorbitol, maltitol, xylitol, and isomalt for pharmaceutical formulations. With over 30 years of expertise and a state-of-the-art facility in Zhaoqing, China, we serve global clients with consistent quality, regulatory compliance, and reliable supply. Our polyols enhance drug stability, taste, and patient compliance. Backed by ISO and HACCP certifications, we ensure every batch meets stringent pharmacopeia standards. Partner with us for tailored solutions, competitive pricing, and dedicated support.
Get A Quote
Advantages of the product

Uncompromising Quality and Regulatory Compliance

Our pharmaceutical polyol excipients are manufactured under cGMP and meet USP/EP/BP standards. Each batch undergoes rigorous testing for purity, microbial limits, and heavy metals. We provide full documentation, including COA, MSDS, and regulatory support for global filings. Our ISO 9001, ISO 22000, and HACCP certifications guarantee consistency and safety.

Extensive Product Portfolio and Customization

We offer a comprehensive range of polyols—sorbitol, maltitol, xylitol, isomalt, and more—in various grades and particle sizes. Our R&D team collaborates with clients to tailor products for specific applications, such as direct compression, wet granulation, or liquid formulations. Custom packaging and private labeling are available to meet your branding needs.

Global Supply Chain and Reliability

With over 33 years of experience and exports to 60+ countries, we have a robust supply chain and strategic inventory management. Our Zhaoqing plant ensures stable production capacity, and our logistics team guarantees timely delivery. We are a trusted partner for pharmaceutical companies seeking a dependable polyol excipient supplier.

Related products

As a premier Pharmaceutical Polyol Excipient Supplier, we understand the critical role excipients play in drug efficacy, stability, and patient acceptability. Polyols, such as sorbitol, maltitol, xylitol, and isomalt, are increasingly favored in pharmaceutical formulations due to their low glycemic index, non-cariogenic properties, and excellent compatibility with active ingredients. Our products are manufactured using advanced hydrogenation technology, ensuring high purity and consistent particle size distribution. We adhere to stringent quality control measures, from raw material sourcing to final packaging, to meet the demanding requirements of the pharmaceutical industry. Our team provides technical support for formulation challenges, helping clients optimize taste-masking, tablet hardness, and moisture control. By choosing us, you gain a partner committed to innovation, quality, and supply chain excellence, ensuring your products reach the market faster and safer.

Frequently Questions

What are the key quality certifications for your pharmaceutical polyol excipients?

Our products are manufactured under cGMP and meet USP/EP/BP standards. We hold ISO 9001, ISO 22000, and HACCP certifications. Each batch comes with a Certificate of Analysis (COA) and Material Safety Data Sheet (MSDS).
Yes, we offer customization in particle size, purity, and packaging. Our R&D team works closely with clients to tailor products for specific applications, ensuring optimal performance.
Standard lead time is 2-4 weeks after order confirmation, depending on quantity and customization. We maintain strategic inventory for urgent requests.
Absolutely. We provide regulatory documentation and support for drug master files (DMFs) and other submissions to help you navigate global regulatory requirements.
We implement rigorous quality control at every production stage, from raw material testing to final product analysis. Our advanced analytics and traceability systems guarantee batch-to-batch consistency.

Related article

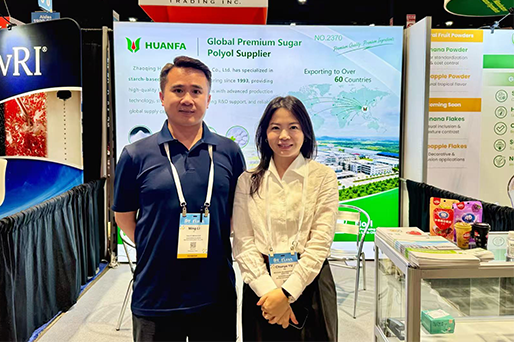
Huanfa Biotechnology Shines at IFT FIRST 2026 in Chicago, USA

18

Aug

Huanfa Biotechnology Shines at IFT FIRST 2026 in Chicago, USA

Huanfa Biotechnology showcased starch-based sweeteners & sugar alcohols at IFT FIRST 2026 Chicago, backed by 33+ years of corn deep-processing expertise.
View More
Why Choose Polyol Sweetener for Your Product?

24

Sep

Why Choose Polyol Sweetener for Your Product?

Polyol sweetener brings low glycemic load and bulk without sugar. See a bakery reformulation, risk points, standards, and a use and care guide.
View More
How to Source High Fructose Corn Syrup from a Reliable Supplier?

24

Sep

How to Source High Fructose Corn Syrup from a Reliable Supplier?

High fructose corn syrup wholesale buying needs more than a low quote. See a blend drift case, risk points, standards, and a sourcing checklist.
View More
Can Sorbitol Powder Be Used in Chemical Synthesis?

14

Sep

Can Sorbitol Powder Be Used in Chemical Synthesis?

Sorbitol powder for chemical synthesis works as a building block and reducing agent. See a real lab case, risk points, quality checks, and supplier tips.
View More

Customer Testimonials

Dr. Emily Carter
Reliable Partner for Our Pharmaceutical Needs

We have been sourcing sorbitol and maltitol from this supplier for over five years. Their consistent quality and timely delivery have been instrumental in our production. Highly recommended.

Mr. Hiroshi Tanaka
Exceptional Customization and Support

Their team worked closely with us to develop a custom xylitol grade for our chewable tablets. The technical support and documentation were outstanding. A truly professional supplier.

Get a Free Quote

Our representative will contact you soon.
Email
Mobile/WhatsApp
Name
Company Name
Message
0/1000
Superior Purity and Safety Standards

Superior Purity and Safety Standards

Our pharmaceutical polyol excipients are produced under strict cGMP conditions, ensuring the highest purity levels. We utilize advanced purification technologies to remove impurities and contaminants, meeting USP/EP/BP monographs. Each batch is tested for heavy metals, microbial limits, and residual solvents. Our commitment to safety ensures that your formulations comply with global regulatory requirements, protecting patient health and your brand reputation. With full traceability from raw materials to finished products, we provide peace of mind.
Innovative Solutions for Formulation Challenges

Innovative Solutions for Formulation Challenges

We go beyond supply, offering formulation expertise to help you overcome challenges such as moisture sensitivity, compressibility, and taste masking. Our R&D team continuously develops new polyol grades and blends to enhance drug performance. Whether you need a specific particle size for direct compression or a low-hygroscopic grade for effervescent tablets, we can tailor our products to your needs. Our collaborative approach accelerates your product development and helps you stay ahead in the competitive pharmaceutical market.

Get a Free Quote

Email
Mobile/WhatsApp
Name
Company Name
Message
0/1000